600 mm Width with Twenty Grooves
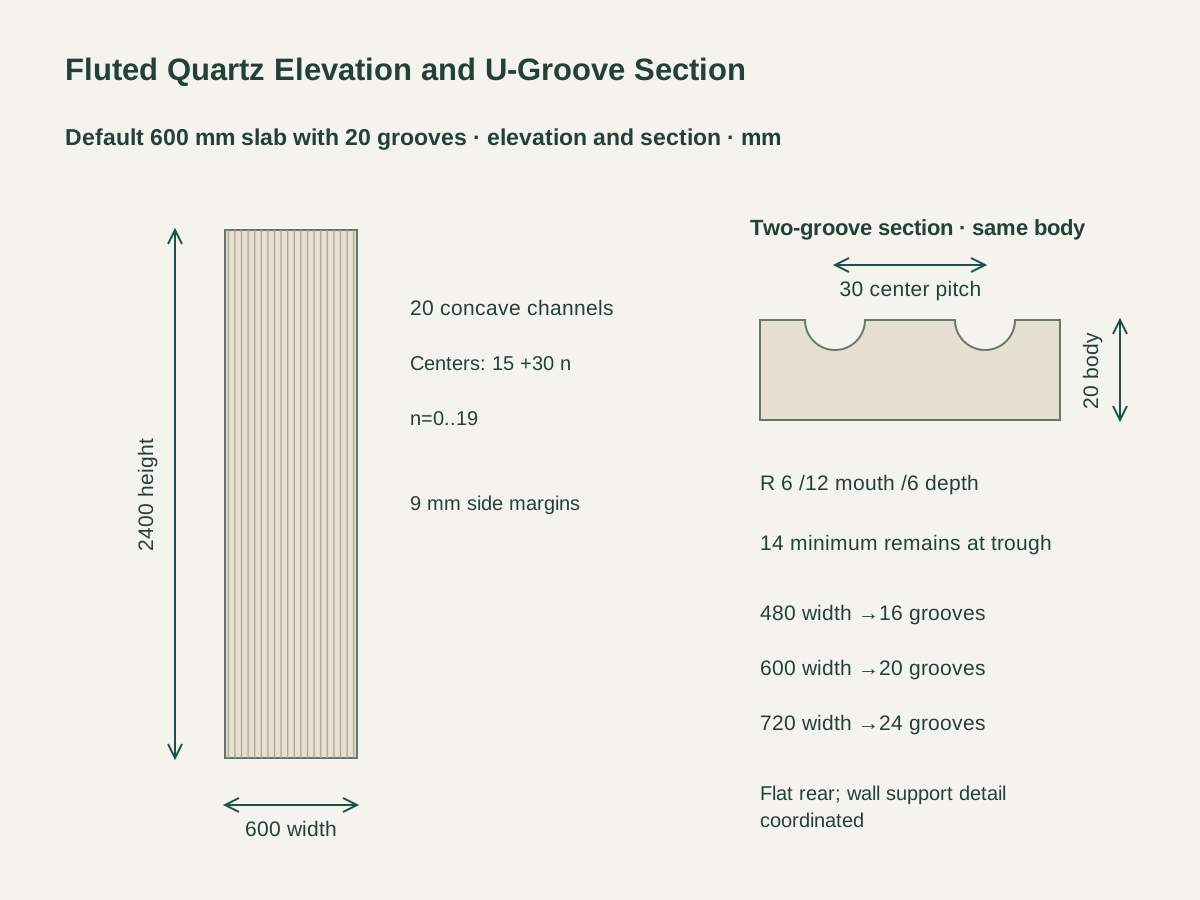
The main 2400 × 600 mm slab has twenty groove centers at 15 +30 n mm across its width. The first and last groove mouths leave 9 mm outer margins on both sides.
Fluted Engineered Quartz Wall Slabs
The warm-white engineered stone uses quartz aggregate in a resin-bound slab. Its matte face, flat rear and 20 mm outer body thickness form the base for the wall-panel machining.
Continuous vertical U-grooves have a 6 mm radius, 12 mm mouth and 6 mm depth. Machining into the front leaves 14 mm of body at each groove trough, with flat lands between the channels.
Groove centers repeat every 30 mm. The rear face is flat for the wall-bond or support detail, and the elevation places panel joints, cut edges and groove direction.
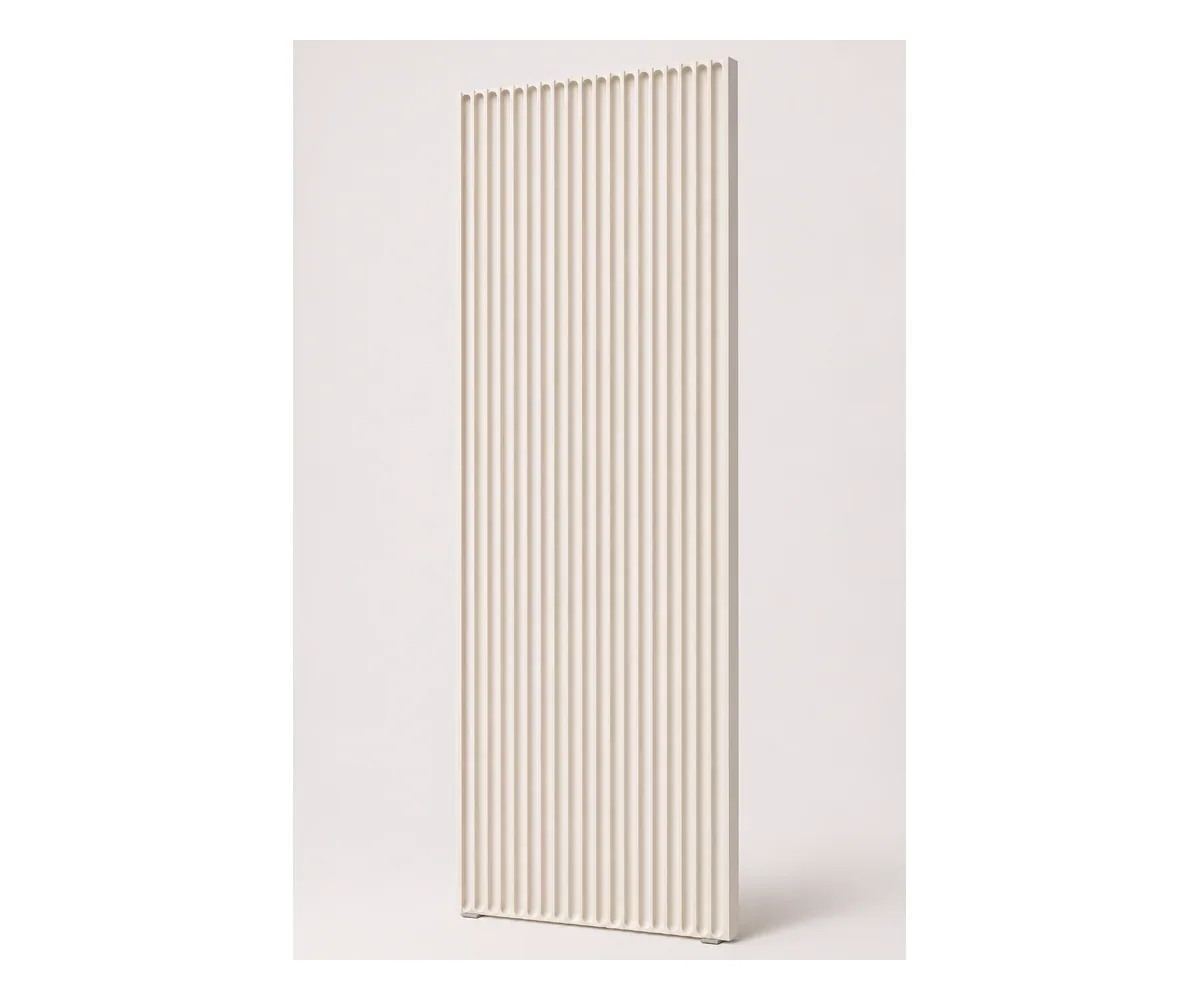
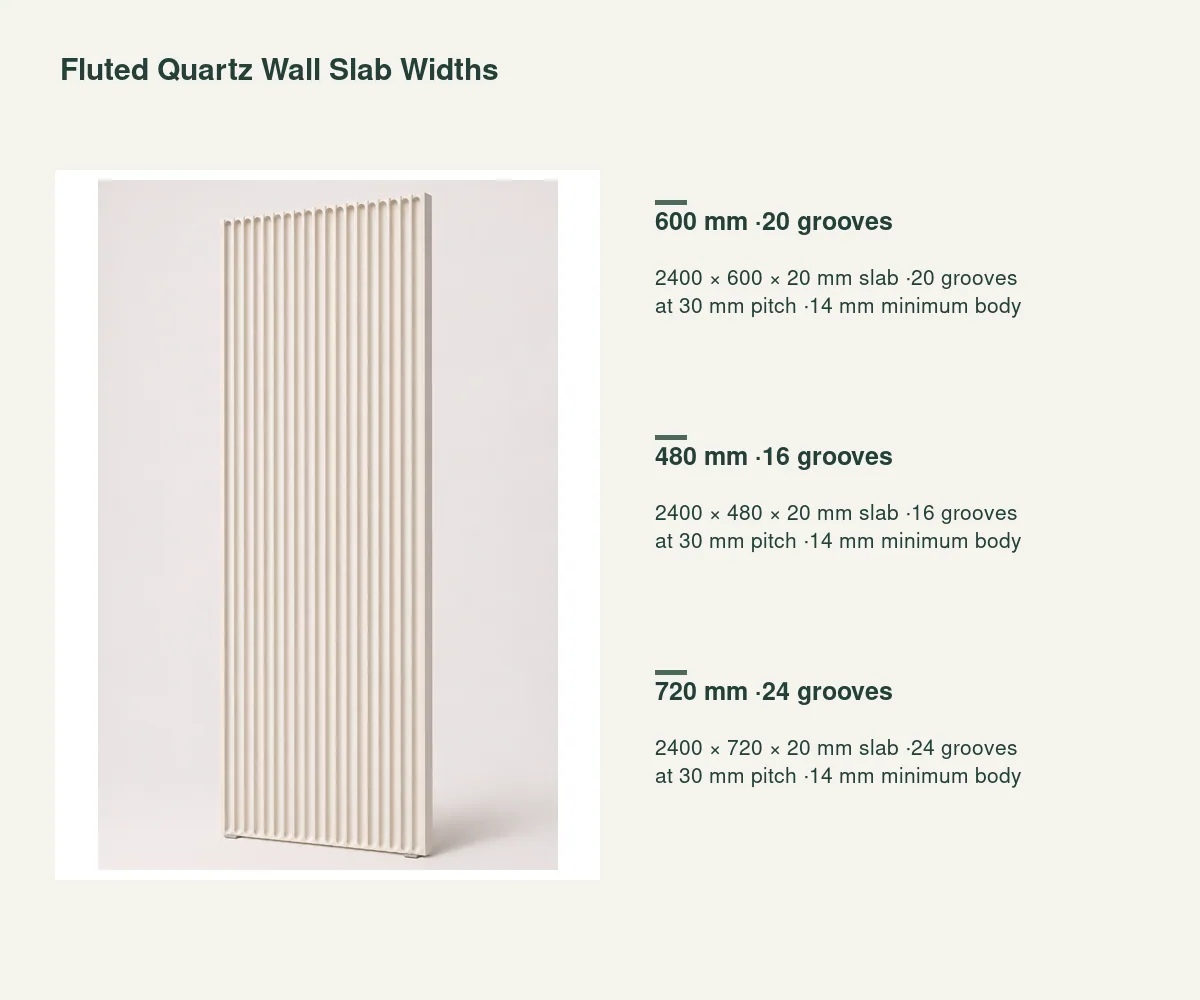
The main 2400 × 600 mm slab has twenty groove centers at 15 +30 n mm across its width. The first and last groove mouths leave 9 mm outer margins on both sides.
The narrower slab carries sixteen channels on the same 30 mm pitch. Its 2400 mm height, 20 mm body and 14 mm minimum trough section remain unchanged.
The wider slab carries twenty-four channels. It retains the same U-section and 9 mm side margins, allowing the wall elevation to compare panel widths without changing the groove rhythm.
| Slab material and face | Quartz-aggregate/resin engineered stone; matte warm white |
|---|---|
| Width and groove count | 2400 × 600 × 20 mm slab ·20 grooves at 30 mm pitch ·14 mm minimum body |
| Height and outer thickness | 2400 H × 20 T mm |
| Concave groove section | R 6 mm; 12 mm mouth; 6 mm depth |
| Pitch and side margins | 30 mm centers; 9 mm uncut outer margin at each side |
| Minimum remaining body | 20 mm body - 6 mm groove = 14 mm at the trough |
| Wall interface | Flat rear; support/bonding, panel joints and cut edges on wall detail |
| Supply unit | One numbered fluted wall slab in chosen width, with face/edge orientation schedule |
 Open product drawing ↗
Vertical channels run through the 2400 mm slab height. The wall drawing locates panel joints, outside edges, returns and openings so groove direction and joint lines remain deliberate across the composition.
The attachment detail matches the stone rear, wall substrate, bonding or mechanical support, and panel dead-load path. Fixing positions and joint widths follow the actual supporting wall design.
The order sample records the matte surface, U-shaped channel, R 6 geometry, edge margins and aggregate, and exposed cuts, returns and handling protection follow the same machined-face reference.
List 480, 600 or 720 mm widths at 2400 mm height. Mark wall locations, cut panels, openings, returns and retained spare material on the elevation.
Quote the 20 mm engineered-quartz slab, R 6 concave channels, 12 mm mouths, 6 mm depth and 30 mm pitch. The 14 mm minimum remaining body stays on the fabrication section.
Itemize bonding/support components, substrate interfaces, panel joints and exposed-edge treatments. The attachment design and machined slab schedule use the same panel numbers.
Protect the groove mouths, flat lands and long slab edges. Mark panel orientation, wall/elevation references, crate counts and destination on the delivery list.
The vertical U-channels are machined into the engineered-quartz front face. Each has a 6 mm radius, 12 mm mouth and 6 mm depth, with flat lands between the grooves.
The 480, 600 and 720 mm slabs contain sixteen, twenty and twenty-four channels respectively. All use 30 mm center pitch and 9 mm outer side margins.
The 20 mm outer slab thickness minus the 6 mm groove depth leaves 14 mm at the deepest point. This remaining section is carried on the wall-panel fabrication and support detail.
All three widths use a 2400 mm height and a flat rear face. The wall attachment is coordinated with the substrate, bonding or mechanical support, panel dead load and joint layout.
The wall elevation establishes groove direction, panel numbers, joints, returns and openings. Cut edges and exposed ends are finished to the same accepted machined-face reference.
Send the panel width and count schedule, wall elevation, openings, returns and spare material, plus the quartz and face reference, machining section, attachment method, edge treatment, packing and destination.
 Crystal-Quartz Piece Composite Decorative Slabs
 Calacatta Gold-Style Engineered Quartz Slabs
 Translucent Engineered Quartz Slabs for Backlit Panels
 Quartzite Shower Bench Seat and Apron Sets